Measuring task and principle
For seamless tubes, wall thickness determines quality and material usage. If it is only checked after cooling in the finishing area, defects have long since spread across many tubes. Measuring directly after the mill is therefore valuable.
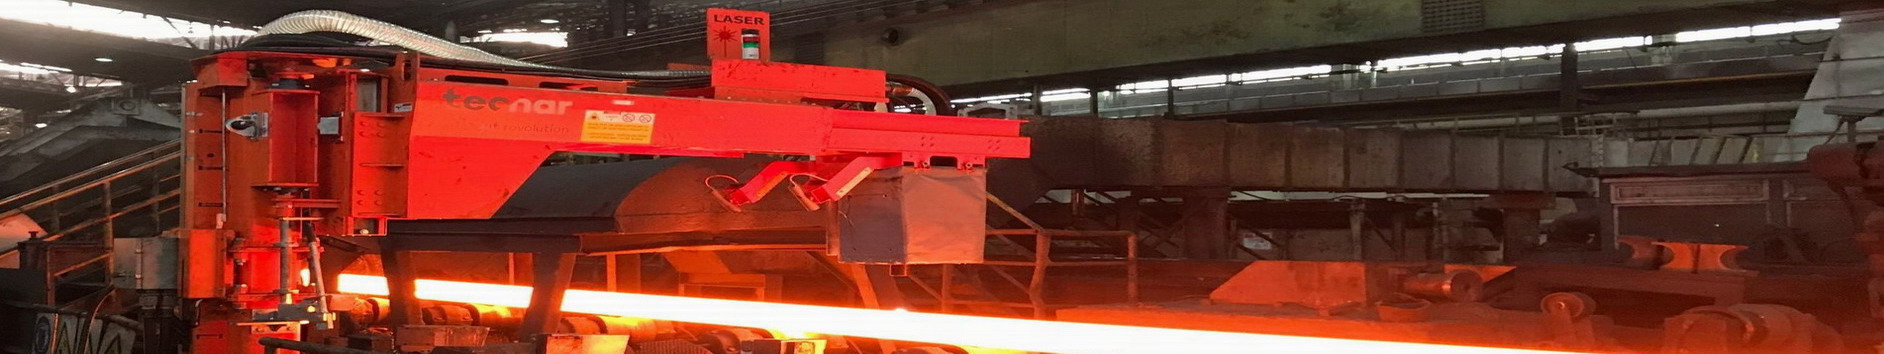
Laser-ultrasonic technology (LUT) makes this possible: a pulsed laser generates an ultrasonic pulse at the hot tube surface, and a second laser with an interferometer detects its echo from the inner wall. The time of flight gives the wall thickness, without contact, without couplant and at rolling temperature.
Applications
Seamless tube mills
Measurement directly after the elongating or sizing mill, in the hot area of the plant.
Detect eccentricity
Wall thickness distribution around the circumference reveals eccentricity and rolling defects early.
Mill set-up
Fast feedback after size changes and during start-up.
Quality documentation
Wall thickness data for every tube as quality evidence.
Benefits
Measurement at rolling temperature
Results are available while the next tube is being rolled.
Less scrap
Defects are detected before many tubes are affected.
Material savings
Tighter wall tolerances allow rolling closer to the lower limit.
Non-contact, no couplant
No water, no contact, no wear on the tube.
Tecnar develops optical and laser-based measuring and inspection systems for industry, including laser-ultrasonic systems for tube production.